Authorised Indian Partner / Applicator for Tecnologic 3 · Italy
Home About Technology Threadlockers Sealants Nylon Locking Patch Anti-Seize & Lubricants Process Quality Applications Contact Request a Quote
Home/Quality & Testing

Performance must be measured.

A pre-applied threadlocker is not simply a coloured patch on a bolt. Its performance must be verified — and breakaway and prevailing torque are measured against specification before any batch is released.

Our Inspection Approach

Five checks between application and release.

01 · TORQUE

Breakaway torque

The torque required to initiate movement of the fastener — the direct measure of the locking function.

02 · TORQUE

Prevailing torque

The resistance generated while the fastener continues to rotate — verified against the applicable specification.

03 · PATTERN

Application pattern

Verification of the treated thread area: band position, length and coverage.

04 · VISUAL

Coating appearance

Visual inspection for consistent, defect-free application on every production run.

05 · RECORDS

Batch traceability

Production and inspection records maintained against the applicable batch — traceable from dispatch back to process parameters.

OBJECTIVE

Same fastener. Same application. Same performance.

Every batch. Controlled and verified.

Quality Control Flow

Every batch. Controlled and verified.

Incoming material→ Process parameter control→ Application control→ Curing / setting→ Visual inspection→ Torque testing→ Batch documentation→ Final release
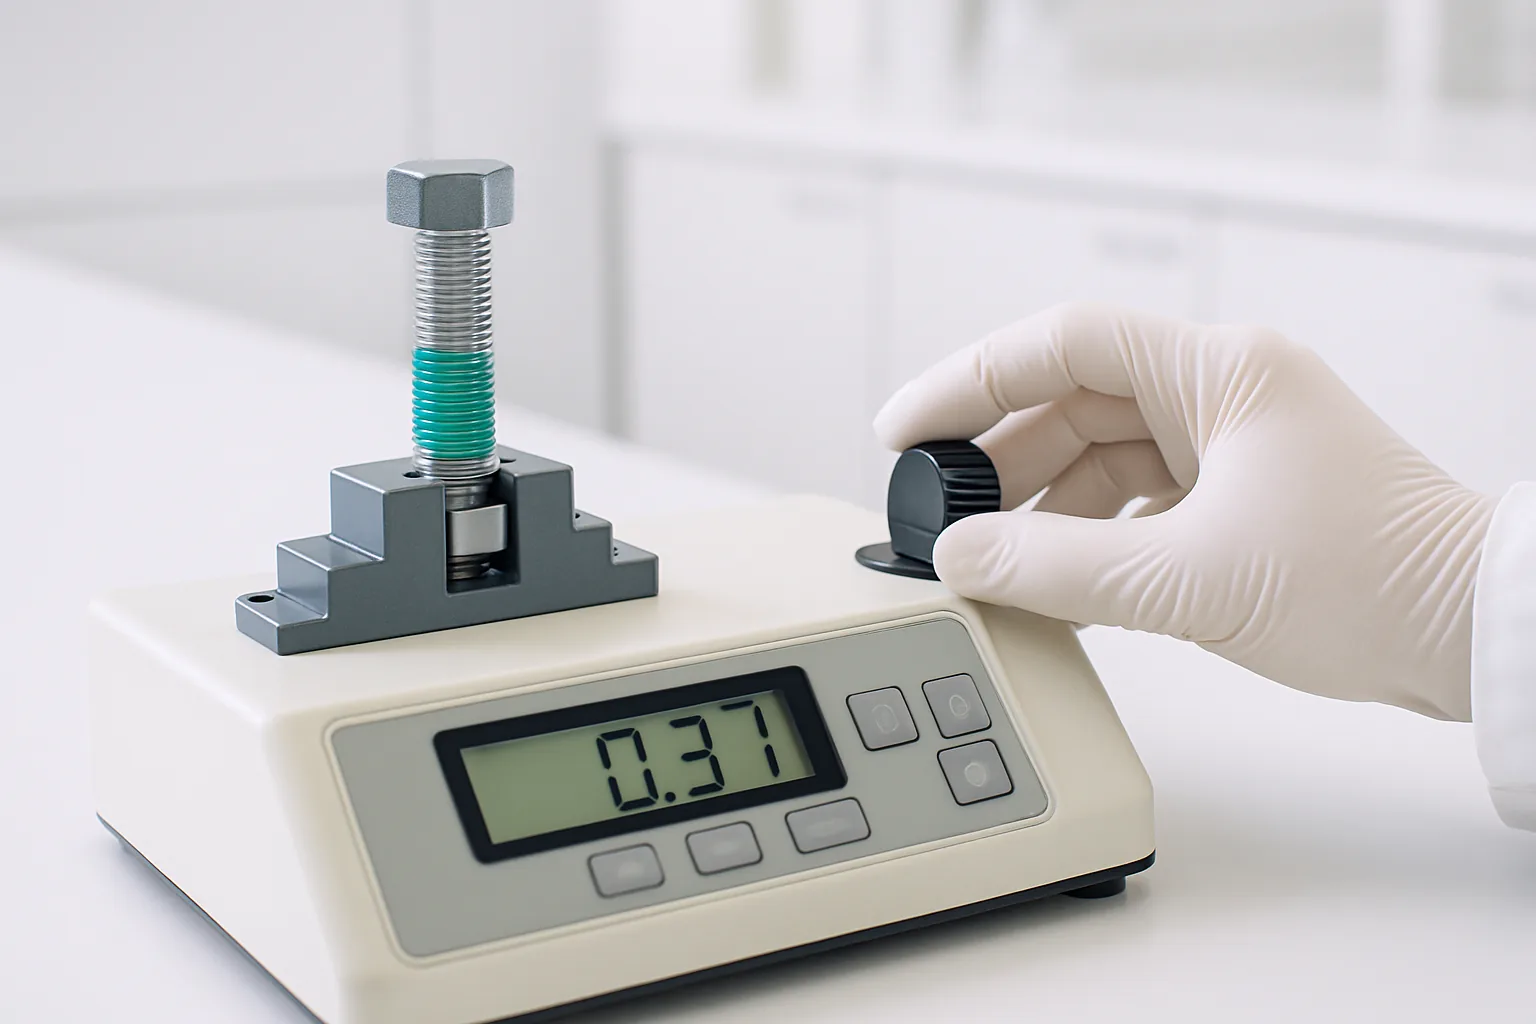
Digital torque testing station measuring a coated bolt

Need torque data you can put in a PPAP?

Tell us your specification — breakaway, prevailing, or your OEM standard — and we will test against it.